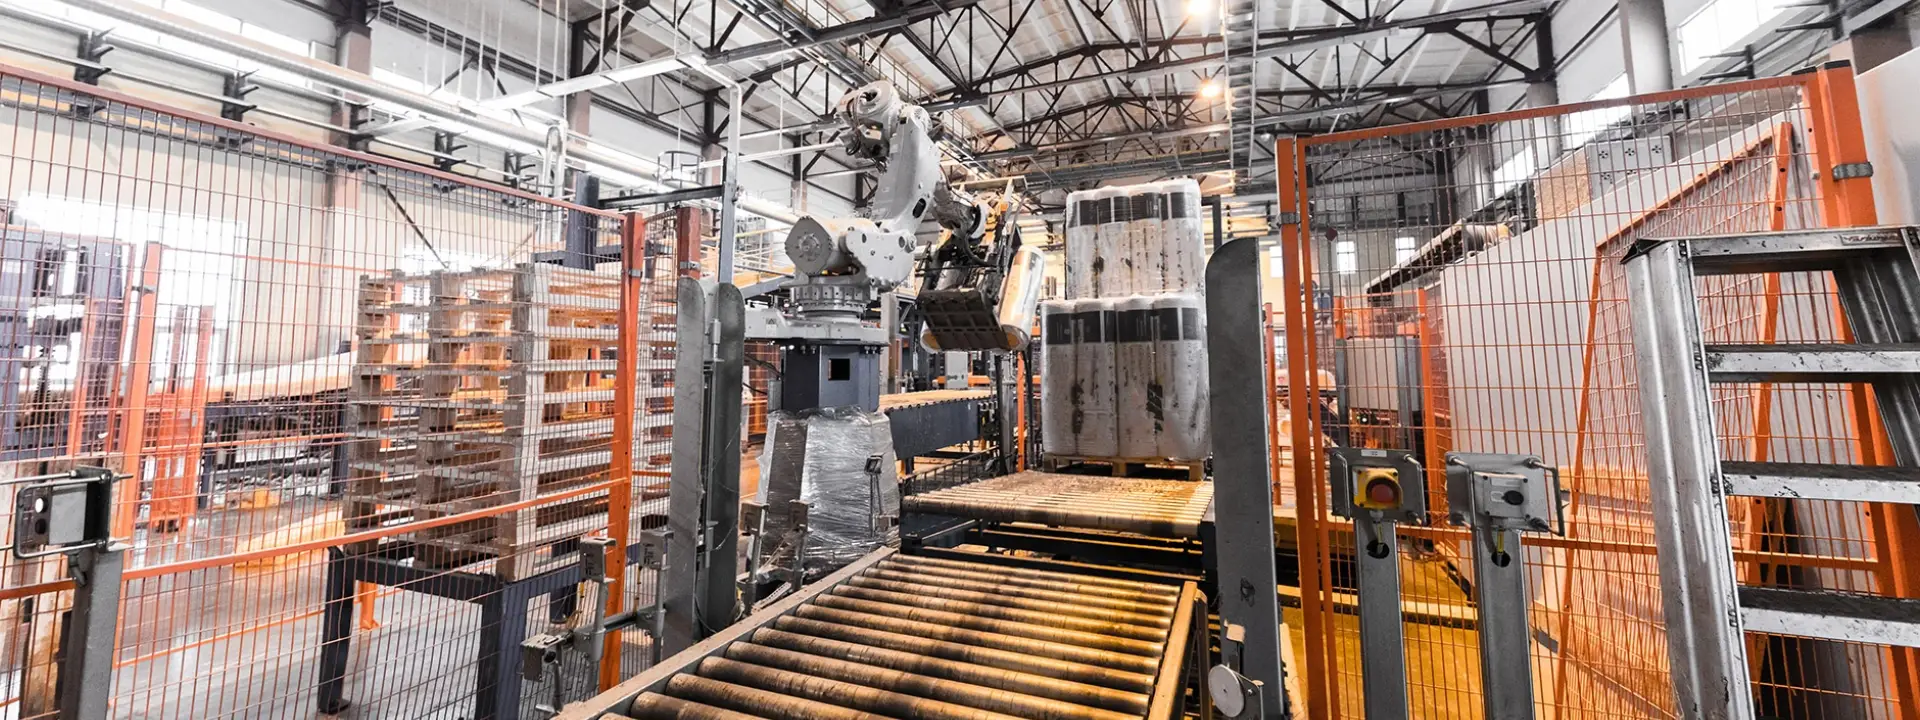
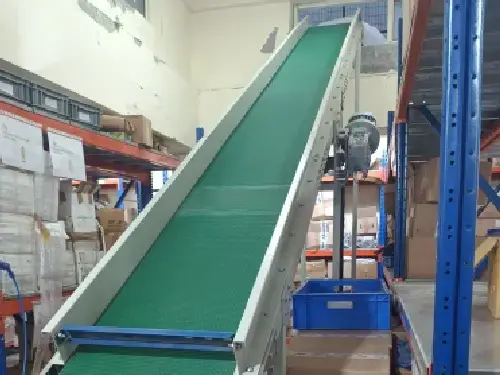
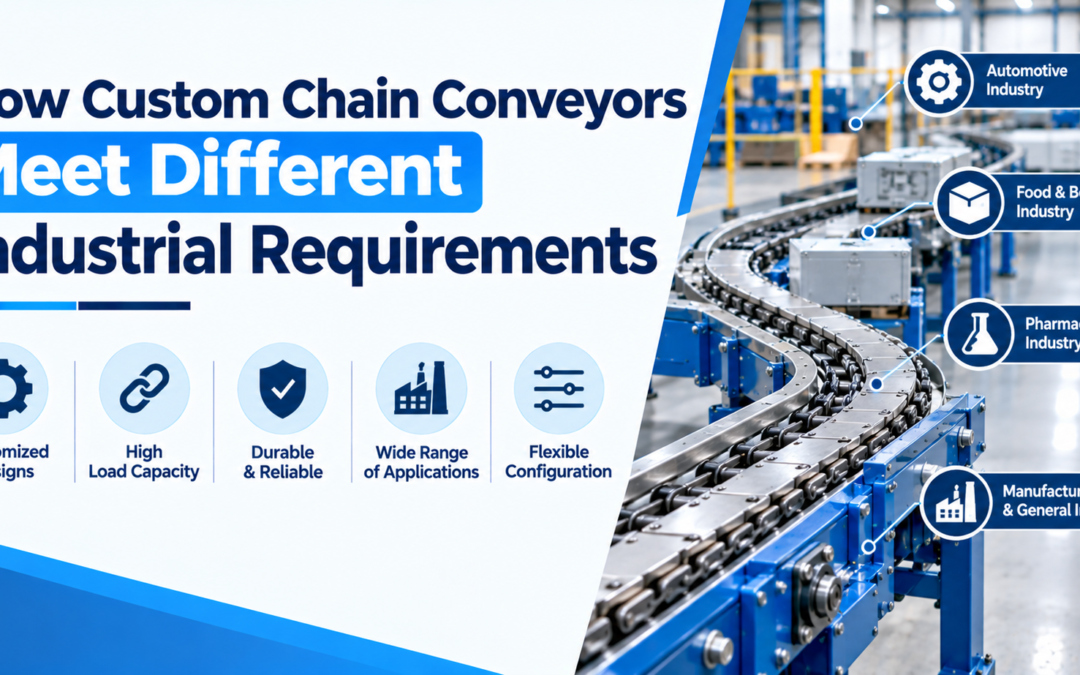
Material handling systems play a crucial role in helping industries maintain efficient operations and smooth production workflows. From transporting components between workstations in the automotive sector to moving products in food processing plants and warehouses, every industry has unique material handling requirements. Businesses can customize chain conveyors to meet their specific needs through flexible designs, load capacities, and configurations.
Custom chain conveyors offer several advantages over standard conveyor systems because they accommodate different material sizes, weights, and operating conditions. SRG Autosolution provides reliable material handling solutions that help industries overcome production challenges, improve operational efficiency, and maintain dependable performance.
What’s a personalized Chain Conveyor?
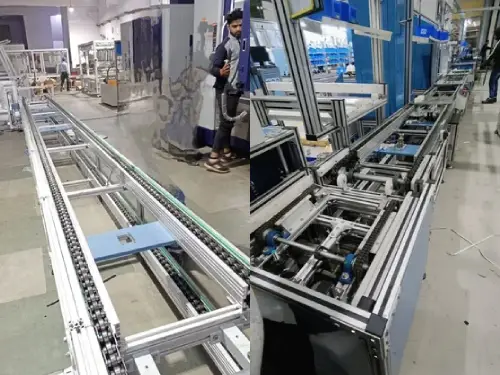
A custom chain conveyor uses a chain-driven mechanism to transport products, heavy loads, and components along a predefined path. These conveyors suit applications that require controlled product movement, efficient load handling, and continuous operation.
Businesses can customize conveyor length, width, chain design, drive systems, and supporting structures to meet their operational needs. Experienced chain conveyor manufacturers consider load capacity, production speed, operating conditions, and available floor space when designing a conveyor system.
Custom chain conveyors offer flexibility for both basic material handling tasks and complex industrial manufacturing lines. Their adaptable designs help businesses optimize production workflows and improve material handling efficiency.
The versatility of Custom Chain Conveyors in addressing various industrial requirements.
1. Handling Different Loads and Materials
Each industry processes materials of varying shapes and size and different weights. In some cases, production lines are used to transport lightweight components and in other cases heavy automotive parts, metal products or industrial containers.
The correct chain, frame, and drive machine can be chosen to meet the specified load requirements for custom chain conveyors. Choosing the appropriate parts helps ensure reliable system performance while reducing idle load.
When deciding which conveyors to use in the industry, a reliable conveyor chain suppliers can assist businesses with the selection of the right type of chains for the required application, operating environment and life.
2. Supporting Industry-Specific Applications
The conveyor systems required vary from industry to industry. A chain conveyor could be required between assembly stations at an automotive facility. Heavy package or container handling systems may be necessary in warehouses. Heavy package and/or container handling systems may be needed in warehouses. They are suitable for use by manufacturing plants to transport goods at various stages of manufacturing.
Conveyors can be incorporated within workflows with custom designs. These may also contain features like variable guides, specific attachments, etc., and automatic controls to facilitate particular handling operations.
This facilitates companies to enhance materials movement and avoid unnecessary manual handling.
3. Better utilisation of space available
Space constraints are often a problem at a plant. The existing layout or equipment may not allow for a standard conveyor to be used.
Sizes and configurations of custom chain conveyors can be tailored to fit the size and layout of a facility. They can be made in different lengths, sizes, transfer points and configurations to suit operational requirements.
A properly designed layout can minimize the number of material movement distances required, enhance workstation connectivity and increase the order and organization of the production setting.
4. Enhance Conveyor Durability and Reliability
Chains, rollers, bearings, drive systems, and supporting structures all influence conveyor performance. Selecting the right components plays a crucial role, especially in demanding industrial environments.
A reliable conveyor roller manufacturer can supply rollers that match the load requirements, material type, and operating conditions. Proper coordination between rollers and chains helps the conveyor move materials smoothly and consistently.
5. Different Conveyor Technologies integrated
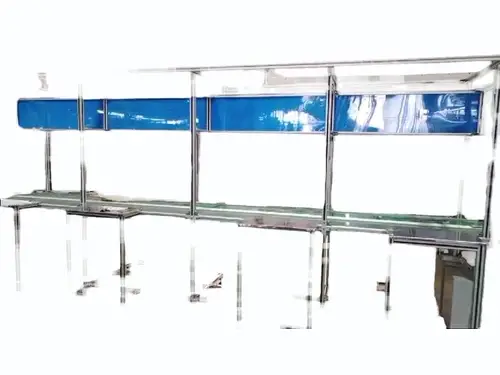
Some production environments require multiple conveyor types to move products quickly and efficiently. Businesses can integrate custom chain conveyors with belt conveyors, roller systems, and other material handling equipment to create a seamless production flow.
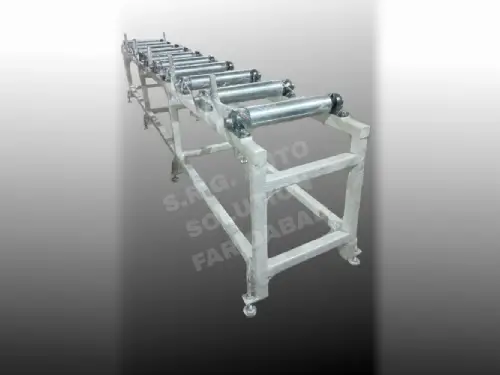
A roller gravity conveyor, for example, moves suitable products between workstations using gravity instead of powered mechanisms. When combined with a chain conveyor, it streamlines product transfers and reduces the need for additional powered equipment where appropriate.
The ideal conveyor combination depends on product weight, shape, transfer direction, and production requirements. Choosing the right combination helps businesses improve material handling efficiency and maintain a smooth workflow.
When selecting a custom chain conveyor, there are a number of factors to take into account.
As businesses consider investing in a custom conveyor system, there are also several key points it needs to take into account:
- Load capacity: Determine the weight and dimensions of the materials being transported.
- Environment: Take in dust, moisture, temperature and other working conditions.
- Production speed: Match conveyor speed with the requirements of the production line.
- Available space: Compatibility – the system must fit into the facility layout and integrate with the equipment already in place.
- Maintenance requirements: Select accessible parts to facilitate easy maintenance and inspection.
- Future expansion: Think about how the conveyor should be expanded if there are changes in the production demand.
Collaborating with a professional conveyor consultant can assist companies in choosing the right conveyor system design for their diverse needs that supports long-term operations efficiently.
Conclusion
Industries can overcome various material handling challenges by choosing custom chain conveyor designs, components, and configurations. As a result, these systems improve load handling, optimize floor space, streamline production workflows, and minimize unnecessary manual transportation.
At SRG Autosolution, we understand the importance of reliable material handling equipment in today’s industrial environment. Therefore, we help businesses identify suitable conveyor solutions by considering load capacity, operating conditions, and production requirements. By taking these factors into account, we provide solutions that support consistent performance, enhance operational efficiency, and maximize productivity throughout the conveyor system’s service life.