In today’s fast-paced business environment, warehouses handle large volumes of products every week. Whether businesses receive raw materials, transport finished products, or manage materials at different stages of production, they need reliable systems to keep materials moving smoothly. Manual handling can consume more time, require additional staff, and create safety concerns. Chain conveyors provide an efficient solution for warehouse and material handling operations.
Chain conveyors can transport products, pallets, containers, and other heavy loads. Their robust construction and reliable performance make them ideal for heavy-duty warehouse and industrial applications.
What is a Chain Conveyor?
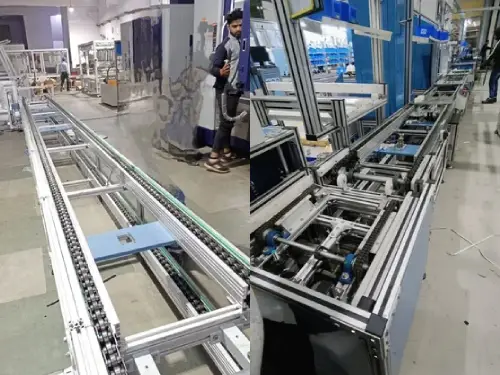
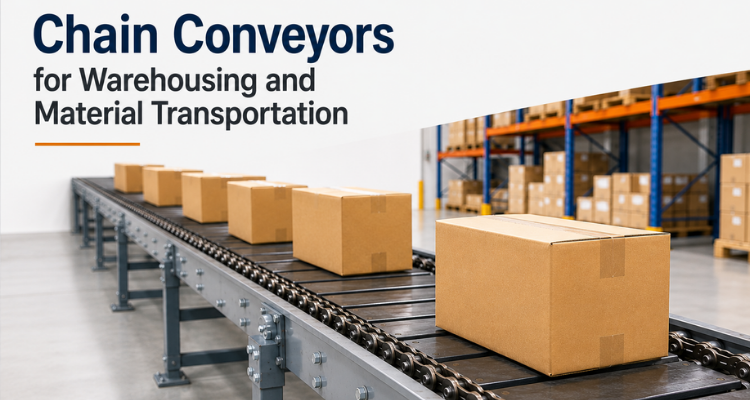
A chain conveyor moves materials from one point to another using one or more continuous chains. The chains run over sprockets, which provide the driving force to move loads along the conveyor system.
Chain conveyors can transport heavier and bulkier products than many conveyor systems designed primarily for lightweight materials. This capability makes them suitable for warehouses, distribution centers, manufacturing units, automotive companies, and other material handling applications.
Manufacturers select different conveyor designs based on load requirements, transport distance, plant layout, and operating conditions. The right design ensures efficient and reliable material movement for each application.
Chain Conveyors in your warehouse have several advantages.
1. Efficient Material Movement
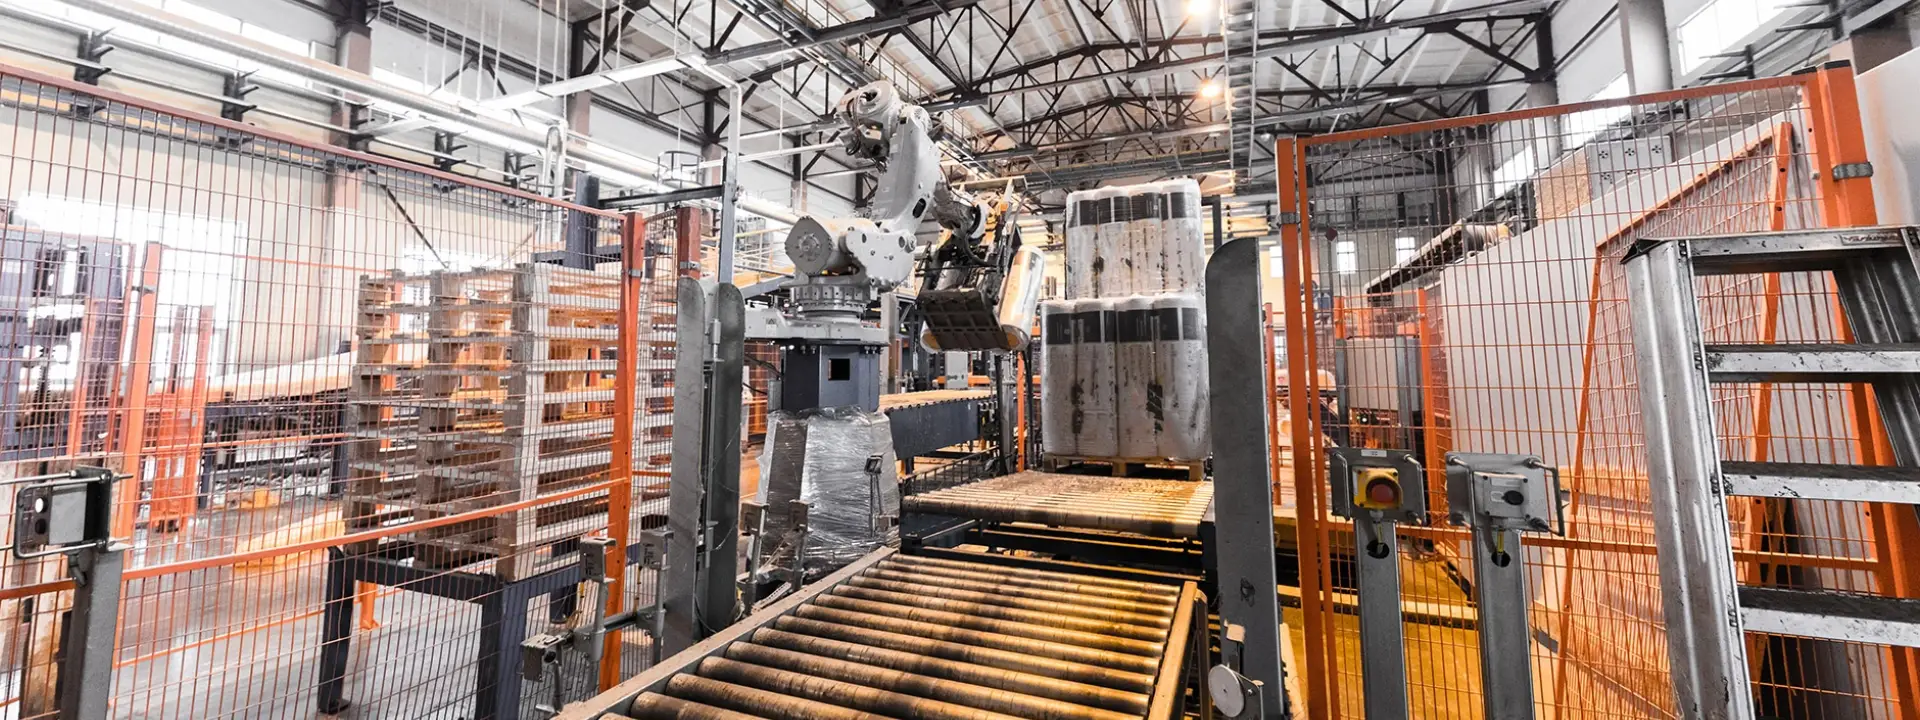
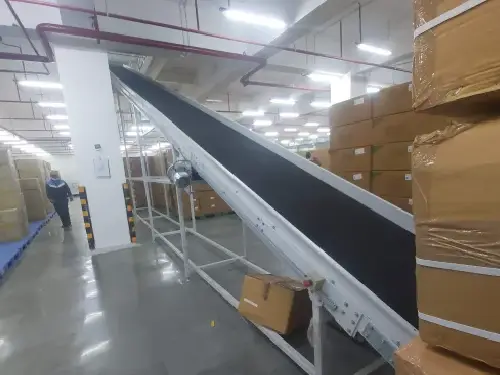
Chain conveyors are used to transport products between various warehouse zones and provide automated retrieval between storage zones with minimal manual participation. They can link up with receiving areas, stores, workstations, packing areas and dispatching.
These can help minimise excessive movement and streamline operations within businesses.
2. Applicable for Heavy Loads
Chain conveyor systems have several benefits, including their capability to move heavy loads. The good quality chains and auxiliary parts enable the system to carry out the following tasks with great effectiveness and efficiency: the moving of pallets, boxes, containers and industrial parts.
Businesses with high load requirements can find the most helpful and experienced chain conveyor manufacturers to get a system that meets their load capacity and operating conditions.
3. Improved Workplace Safety
The risk of workplace injuries and strains may increase with the manual lifting of materials. An effectively designed conveyor system helps eliminate the necessity of employees to lift or carry heavy products repeatedly.
This allows employees to concentrate on other tasks that are important to the warehouse.
4. Flexible Warehouse Integration
It’s possible to combine chain conveyors with various warehouse configurations. They can be used in straight sections, or integrated with other material moving machinery and systems to form an integrated whole.
Conveyors can also be made up to other dimensions, floor space, product size, load, and distance of travel that may be available for specific purposes.
Chain Conveyors vs Roller Conveyors
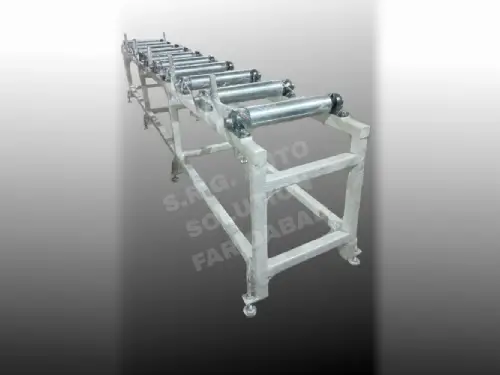
Another common type of transport method in warehouses is roller conveyors. A roller gravity conveyor is a product movement machine that uses the effect of gravity and the roller mechanism to move appropriate products along an inclined or horizontal track. The advantage of these systems is that they can be used for products with relatively flat and stable bases, such as boxes, cartons, cartridges, and totes.
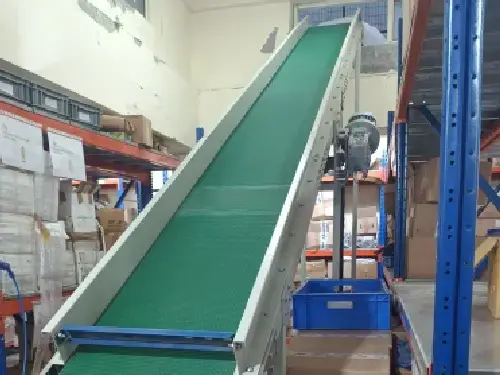
For heavier loads and applications where positive movement is desired, belt conveyors may be preferred. The appropriate selection will depend on the product weight, product shape, the surface they are covered with, the desired speed, the conveyor configuration, and the level of automation needed.
A chain and roller conveyor system can be combined in some facilities for a more efficient handling process.
All conveyor components must be of high quality.
The quality of the parts that make up a conveyor system is crucial for its performance and service life. Chains, sprockets, frames, rollers, bearings and drive systems need to join forces with efficiency.
If the system has rollers, collaborating with a reputable conveyor roller manufacturer can assist in making certain that the rollers are appropriate for the load and operating conditions required.
Likewise, companies should also pick reliable conveyor chain suppliers who can offer sturdy and durable chains corresponding to the application. Unexpected breakdowns, maintenance demands and operating downtimes can be minimized by quality components.
Applications in Warehousing and Material Transportation
The following is a wide range of items that are transported using chain conveyors as a means of transportation:
- Large boxes, bags, cases and cartons used for heavy items.
- Industrial components
- Packaging and pallets.
- Automotive parts
- Manufacturing materials
- Metal products
- Bulk handling units
- Finished products
They can help the cargo flow from storage to the production area, assembly area, packing area and shipping area.
Choosing the Right Chain Conveyor
Businesses should consider several factors before installing a chain conveyor. These include product weight and size, conveyor length, operating speed, available workspace, loading and unloading points, and operating frequency.
Businesses should also evaluate the conveyor’s construction materials, drive mechanism, chain type, safety features, and maintenance requirements. An experienced manufacturer can assess these factors and recommend a suitable conveyor configuration that meets the specific application needs.
Conclusion
In today’s warehouses, chain conveyors offer a reliable and efficient way to move materials. They support various applications because they can handle heavy loads and operate continuously alongside other material handling equipment.
If your business plans to upgrade its warehouse, a well-designed conveyor system can increase productivity, reduce manual handling, and streamline material flow. High-quality components, proper customization, and regular maintenance help chain conveyors deliver reliable performance for many years.