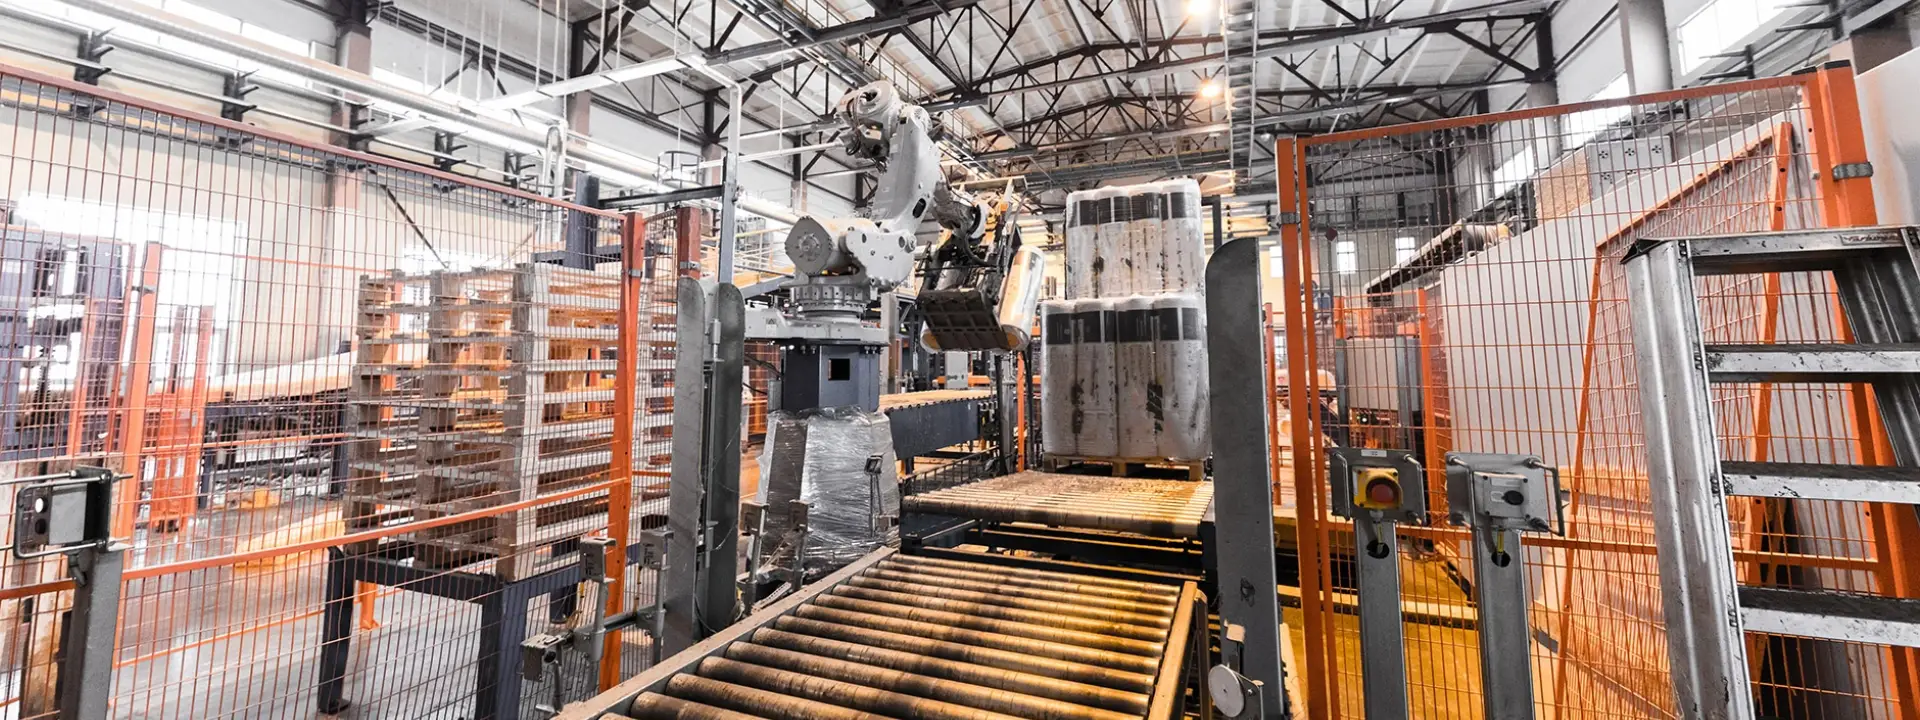
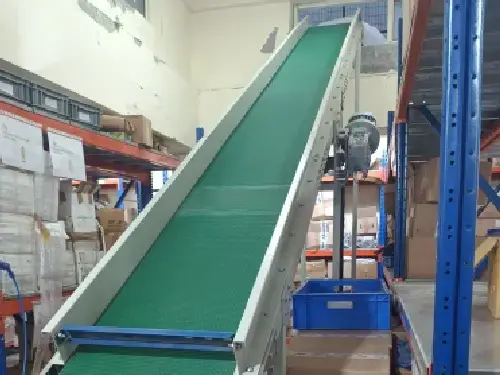
In today’s industries that require efficient manufacturing and material handling, conveyor systems are vital tools in the facilitation of smooth, rapid, and structured operations. Conveyors play a vital role in businesses, helping them to transport raw materials, components, finished products and heavy loads from one process to another in a streamlined way.
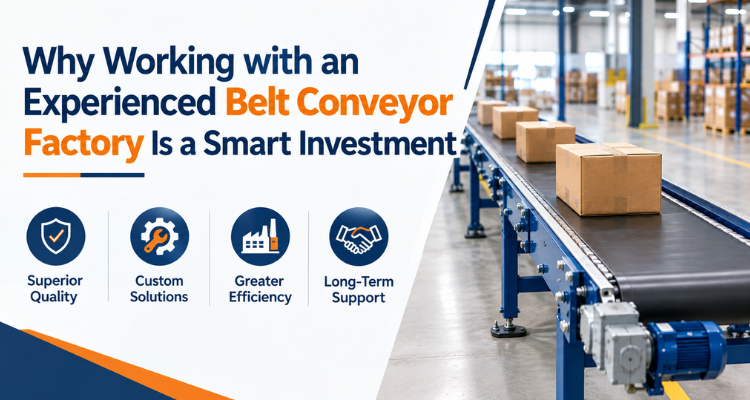
Yet the selection of the right conveyor supplier has the power to impact workplace working productivity, maintenance costs, equipment life and workplace safety. Therefore, collaborating with an established belt conveyor factory can prove to be a wise investment for companies seeking dependable and sustainable material-handling solutions.
1. Increased knowledge of industrial needs.
Material-handling needs in each manufacturing plant vary. Conveyor design can be influenced by load capacity, conveyor length, belt speed, product type, environmental conditions and production volume.
A seasoned manufacturer knows these things and can give you a recommendation on what type of conveyor you should use for your application. A tried and tested manufacturer, rather than providing a generic answer for all projects, will be able to design production-specific equipment.
This can help optimise operation and minimise the risk of achieving a result that is not suitable for the required equipment.
2. Quality Control throughout the process
Seasoned manufacturers typically possess a good amount of comprehension of the various kinds of conveyor technologies and industrial uses. This enables them to offer options for different production environments.
A modular belt conveyor, for instance, may be useful when conveying surfaces need to be durable and easy to maintain for use in applications. The modular belts are built from interlocking parts, helping the individual parts be more easily replaced if needed.
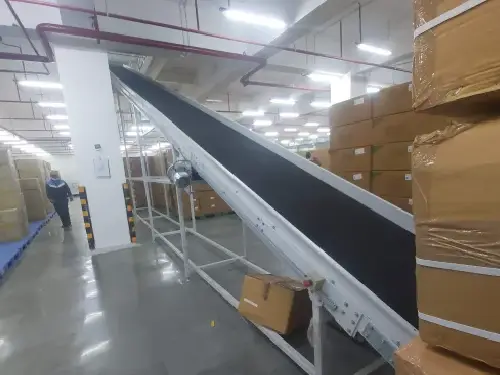
In contrast, a flat belt conveyor can be an effective option for handling packaged goods, parts, boxes and other materials in manufacturing and warehouse plants.
The use of the right design guarantees the smoothness of the flow of materials and the regularity of production is guaranteed.
3. Improved Equipment Quality
That the quality of a conveyor system is dependent on the components, construction, assembly and manufacturing standards of the conveyor system. A savvy producer is knowledgeable about the influence each piece can apply to system performance.
The selection of quality roller, conveyor frames and belts, motors and bearings and supports can also help make a more durable conveyor. Using the correct manufacturing and assembly materials, steps and processes can also minimize the risk of premature failures.
This means companies can rely on equipment that performs consistently under challenging conditions.
4. Customized Conveyor Solutions
Industries rarely have sufficient space for their production needs, or a set of production processes that can be accommodated by the standard floor plan. Not all standard conveyors will necessarily meet these needs.
Foragers with years of knowledge can design a conveyor that fits your needs and requirements, whether you’re working in an apartment, car port, or garage with limited room; or you must convey some goods from place to place to a particular direction. They may also take conveyor angles, transfer points, loading space and discharge points into consideration during the design phase.
Customization can be used to maximise production areas and improve the material flow in the business.
5. Less Maintenance and Downtime
Non-availability of conveyors can disrupt the production process, raising operating expenses. Regular maintenance also puts strain on maintenance teams.
An optimized conveyor system design and production can minimize the need for unnecessary maintenance. After all, well-experienced manufacturers know about typical issues on conveyors, like misalignment, overloading, belt tension problems and poor component selection.
When considering these factors at the design and manufacturing phase, it is possible to minimize unnecessary downtime and achieve more consistent production.
6. Increase Safety and Operational Efficiency
One must always take safety into consideration while choosing the industrial equipment. Operators and maintenance staff should be considered when designing and installing conveyors.
For experienced manufacturers, there are additional considerations to take into account like emergency stops, guards, safe access points, conveyor belt speeds, and positioning.
Meanwhile, a sound conveyor design can enhance workflow and eliminate wasteful manual manpower by minimizing the requirement for manual transport. This can enable workers to concentrate on other productive tasks and facilitate the movement of materials efficiently between workstations.
7. Long-Term Cost Benefits
It’s not always the best investment: the lowest initial purchase price. A cheap conveyor which needs frequent repairs or replacement may eventually end up costing more than a good conveyor system.
Skilful manufacturers understand and balance the short term investment with the long term performance, durability, maintenance and energy needs.
If selected, operated and maintained correctly, a quality conveyor system will provide reliable service for many years. This can facilitate businesses in managing their operating costs and also optimizing them from improving value on investment.
8. Supply of professional support and technical expertise.
Additionally, hiring a manufacturer with experience gives you beneficial technical know-how. Professional input can ease the purchasing process from conveyor selection to installation and maintenance procedures.
A dependable manufacturer can also assist businesses in picking out potential issues before the equipment is set up. This helps to minimise the cost of redesign later.
Conclusion
Making an investment in a conveyor system is a long-term investment which can impact the efficiency of production, material handling, maintenance and operational costs. However, for businesses it is imperative that they look beyond price when they’re considering their choice of conveyor supplier.
If you can work with a manufacturer that has experience in their field, you can reap several benefits from them, which are quality equipment, designs that can be customized, reliability, improved safety and long-term cost savings.